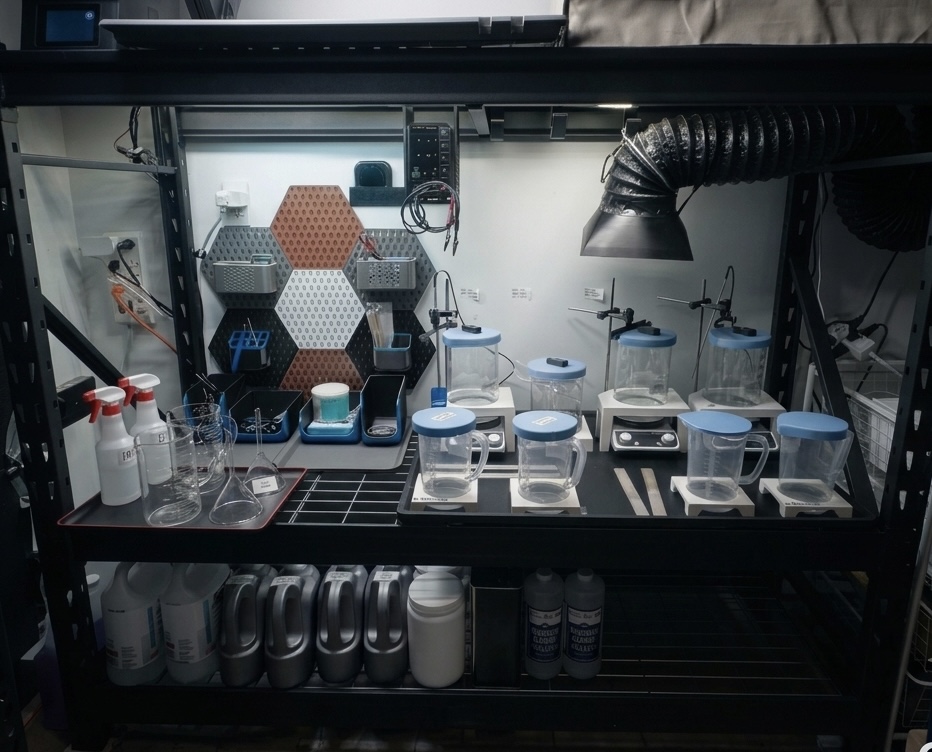
Watch plating is often done on a kitchen counter: the whole watch dipped assembled, movement and all. This is different. K-Plating runs from a dedicated lab with temperature-controlled baths, filtered rinses, a D65 booth for reading colour, CIELAB-proven colour matching, processes validated by X-ray fluorescence (XRF), and a bench for testing hardness and wear, because the things that decide quality should be measured, not assumed.
Nothing here is for show. Each stage exists because skipping it is exactly how a plate fails, in a week, or in a year.
The watch comes apart: movement, dial and hands out, bezel, case-back and crown off, the bracelet taken apart, each part handled and racked on its own. This is the step most commonly skipped: dropping the whole watch in fully assembled instead. A closed watch traps solution, leaves blind spots the current never reaches, and carries oils and old grease straight into the bath, contaminating the chemistry for everything that follows. Loose parts mean the deposit reaches every accessible surface, inside and out, evenly. It is the single biggest reason this work costs more than a dip-it-as-it-sits job, and the single biggest reason it lasts.
A multi-stage clean: two manual cleaning procedures, a purpose-made watch cleaning fluid degrease, ultrasonic isopropyl, an electro-clean, and an electrolytic activation that strips the last invisible oxide layer so the deposit bonds to bare, active metal. This is where most of the time goes, and where most plating jobs quietly fail before they even start.
Not one dip, but a layered structure across multiple gold types, built up to 6 µm where a piece calls for it. The wearing surfaces go down in cobalt-hardened hard-gold, which resists scuffs and edge wear far better than the soft 24K flash most shops finish with.
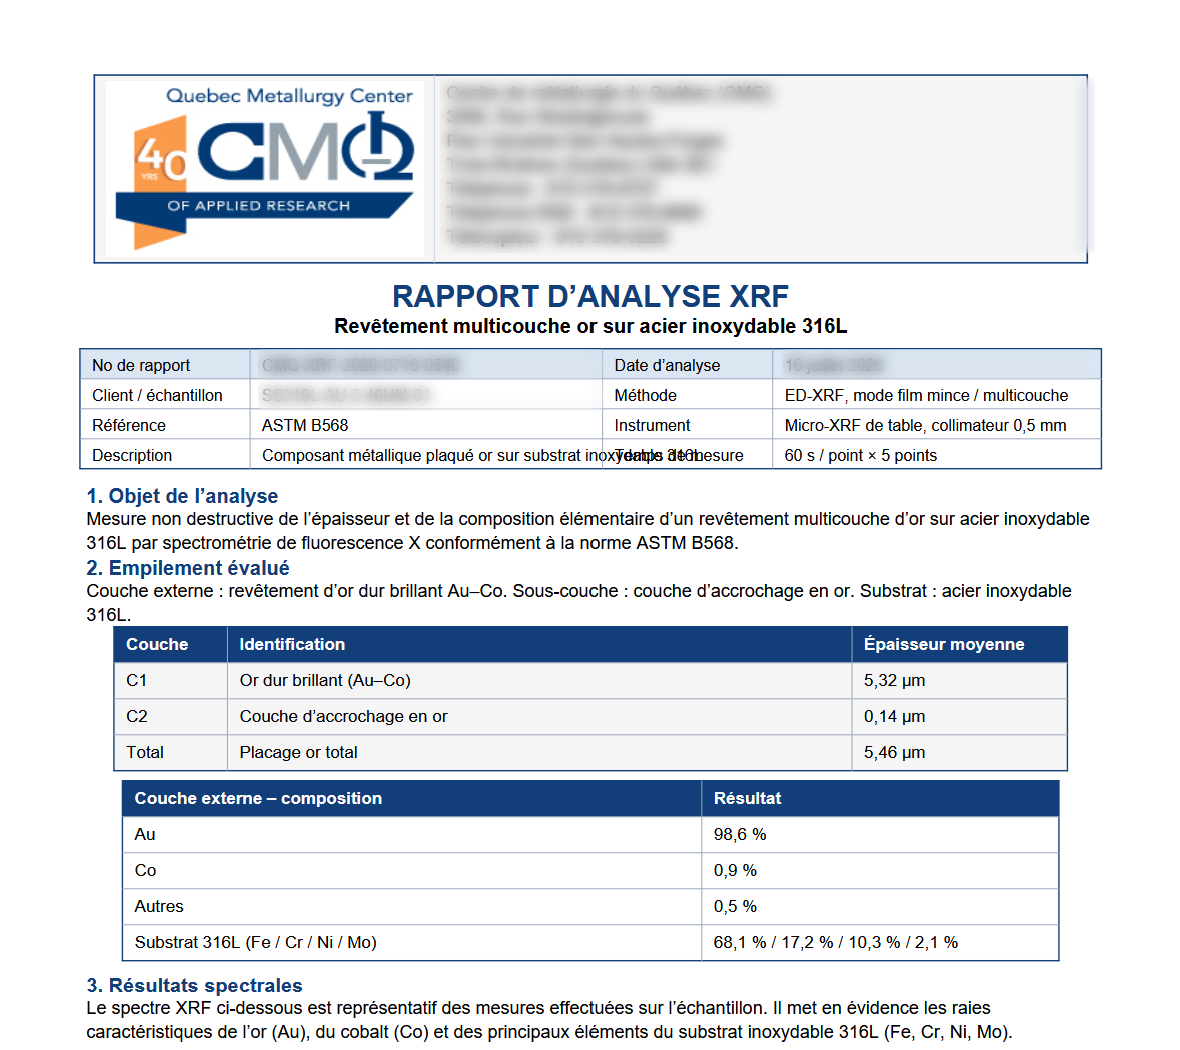
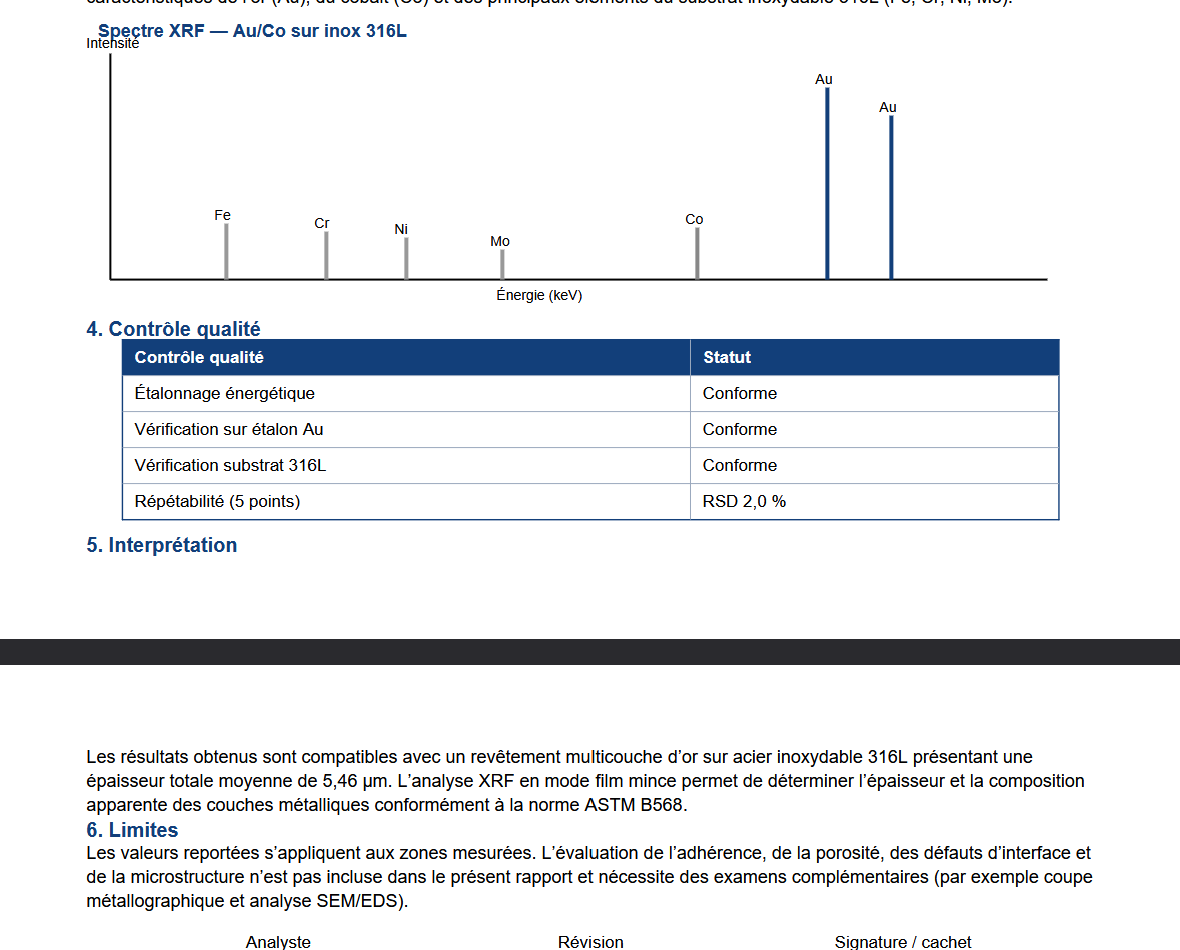
Bath chemistry, current and timing are validated quarterly by independent XRF at an accredited lab, so we know what thickness a given run produces. The XRF validates the process, not each individual watch: your piece is plated to parameters already proven rather than to a number being hoped for. Colour is held to the same standard, quantified by spectrophotometry in CIELAB coordinates so a tone is a measured value with a stated ΔE, not an opinion.
Every piece is checked visually under standardized D65 daylight for tone consistency across the whole assembly, case to clasp. A dedicated hardware spectrophotometer then captures the full reflectance curve of the surface across the visible spectrum, producing an objective CIELAB reading for every scan. The instrument is built with sealed glass optics in an industrial-grade metal enclosure and calibrated against a diagnostic reference tile before every session. It catches what the eye alone cannot: two gold surfaces can look identical under one light but show a visible colour shift under another. Colour is verified both by eye and by data, and every reading is logged to a proprietary colour library that grows with each piece.
A final inspection under magnification, careful reassembly, and a final QC pass. Every watch, tone-matched or not, clears the same finish-quality gate before it ships back, tracked and insured.
“5 microns” gets quoted like a guarantee. It isn’t. A thick deposit over a dirty, un-activated surface peels just as fast as a thin one, sometimes faster. Thickness only matters once everything underneath it is right. Here’s what actually decides whether a plate survives real wear.
A deposit is only as good as its bond to the metal beneath. Proper degreasing and electrolytic activation are what keep gold from lifting at the edges. Skip them and no amount of thickness saves you.
Soft 24K looks great for a week, then scuffs on a desk edge. Cobalt-hardened hard-gold on the wearing surfaces is what lets a finish keep its colour and edges through daily wear. Measured by Knoop microindentation hardness testing (ASTM E384): 234 HK for the gold, several times harder than ordinary soft gold plating.
In electroplating, the metal builds up wherever the electrical current is strongest, and that current naturally concentrates on outer edges and corners while thinning out inside tight recesses. Left alone, that means bald, under-plated spots deep in the lug slots and between links. To counter it, we plate the watch fully disassembled and rack each component individually, positioning and spacing every part so the current reaches into the recesses instead of racing around the outside. The result: the hidden interiors get the same gold thickness as the flat, easy-to-reach faces.
On Rolex, tone is checked visually under controlled D65 illumination against modern genuine Rolex, so the gold reads right in daylight, not just under a warm bulb that flatters everything. A spectrophotometer then captures the full reflectance curve and reports an objective CIELAB reading, catching shifts between lighting conditions that no eye can. The match is measured and seen, not one or the other.
Nickel is a widely used underlayer in gold plating, in both watches and jewellery. Nickel is cheap, it levels a surface beautifully, and it makes a convenient diffusion barrier. It is also one of the most common contact allergens in the world, and it sits directly against skin on a watch case-back and bracelet, the two highest-contact surfaces on any object most people own.
Regulators treat it accordingly. Under EU REACH Annex XVII, articles in prolonged contact with skin are restricted by nickel release rate, and jewellery and watch components fall squarely inside that scope. A gold layer over nickel is one wear-through away from putting nickel on skin, and the wear-through happens exactly where you would expect: clasp edges, lug tips, bracelet link flanks.
No nickel underlayer is intentionally applied. Beneath the gold sits a precious-metal barrier layer, harder than the gold above it and metallurgically stable against diffusion. It costs a multiple of what nickel costs, and it removes the most commonly reported contact allergen from the plating layers.
The gold is built up in multiple layers; the wearing surfaces include cobalt as a hardening agent (assayed at 98.6% Au, balance cobalt), and no nickel is intentionally introduced at any stage. That is most of the difference in the price. Note that the underlying watch case and bracelet (typically 316L stainless steel) contain nickel as an alloying element; individual skin sensitivities vary.
The deposit is built on a sliding scale up to 6 µm, set by the tier you choose and quoted per piece. Thickness is controlled by charge (current density and time per surface area) and the process is validated quarterly by independent XRF at an accredited lab. Gravimetric methods are used alongside XRF to confirm the gold you paid for is on the watch. Hardness is measured, not asserted. Knoop microindentation hardness testing (ASTM E384) puts the cobalt-hardened gold at 234 HK, several times harder than ordinary soft gold plating, which is what keeps edges and colour through daily wear. Adhesion and wear resistance are also demonstrated on camera: a screwdriver dragged across the surface, acrylic glue pulled off it, and 3M tape lifted from it. What you get is a finish built to a standard you can be shown, not just told.
Tell us what you’ve got. A $25 deposit holds your place on the bench.